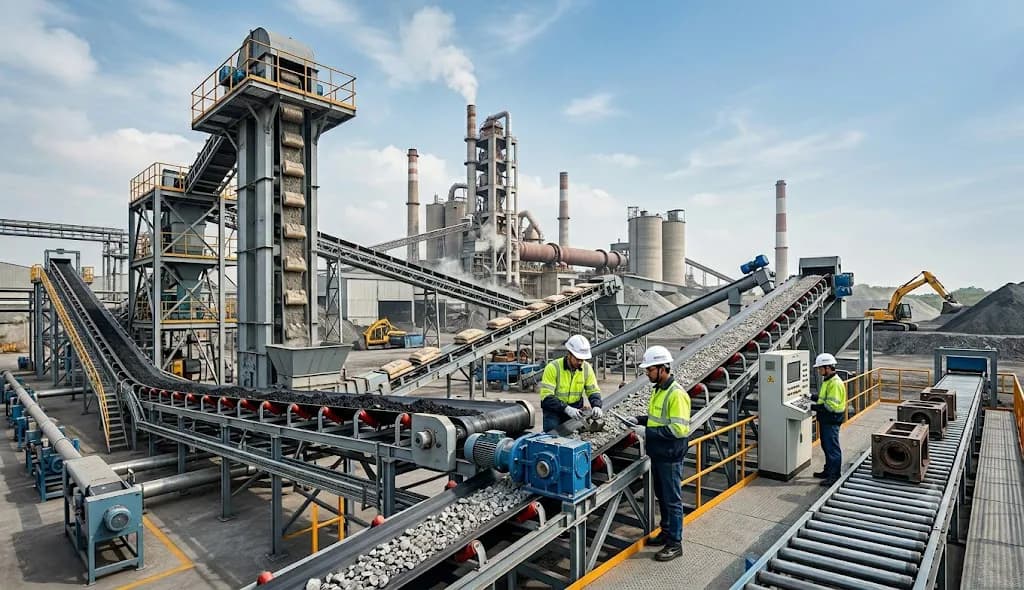
Engineering Productivity Through Reliable Conveyor and Material Handling Systems
Industrial growth depends heavily on the efficient movement of materials. Whether it is a manufacturing plant, power generation facility, cement unit, mining operation, or processing industry, the ability to transport bulk materials safely and efficiently has a direct impact on productivity and operational costs.
This is where METLRG SOLUTIONS plays a significant role. Specializing in the manufacture and supply of high-performance material handling equipment, the company provides a comprehensive range of products including Belt Conveyors, Bucket Elevators, Chain Conveyors, Screw Conveyors, Ash Conditioners, Roller Conveyors, Sector Gates, Rack & Pinion Gates, Rod Gates, and Conveyor Spares. Designed to meet demanding industrial requirements, these solutions help businesses streamline operations while maintaining reliability and safety.
Why Material Handling Equipment Matters More Than Ever
As industries continue to expand production capacities and automate processes, efficient material movement has become a critical component of operational success.
Poorly designed conveying systems can lead to:
Production bottlenecks
Material wastage
Increased maintenance costs
Equipment downtime
Workplace safety concerns
Modern industries require robust systems capable of handling heavy loads, abrasive materials, and continuous operations. METLRG SOLUTIONS addresses these challenges through engineered products that are built for durability, efficiency, and long-term performance.
Comprehensive Product Portfolio for Diverse Industries
One of the key strengths of METLRG SOLUTIONS is its ability to provide multiple material handling solutions under one roof.
Belt Conveyors for Continuous Material Transport
Belt conveyors remain one of the most widely used systems across industries. They offer efficient transportation of bulk materials over long distances while reducing manual handling requirements.
METLRG SOLUTIONS manufactures belt conveyors designed for:
Mining operations
Cement plants
Power plants
Fertilizer industries
Food processing facilities
Warehousing and logistics sectors
These systems are engineered to deliver smooth operation, high load capacity, and reduced maintenance requirements.
Bucket Elevators for Vertical Material Handling
Moving materials vertically presents unique challenges. Bucket elevators are specifically designed to transport bulk materials efficiently between different elevations.
Applications include:
Grain handling
Cement manufacturing
Chemical processing
Mineral processing plants
The bucket elevators supplied by METLRG SOLUTIONS provide reliable performance, minimal material loss, and efficient vertical transportation.
Chain Conveyors for Heavy-Duty Applications
For industries handling heavy and abrasive materials, chain conveyors offer a dependable solution.
Key benefits include:
High durability
Ability to handle harsh environments
Long operational life
Consistent performance under heavy loads
These systems are particularly valuable in power generation, mining, and bulk material handling industries.
Specialized Solutions for Challenging Industrial Environments
Every industry faces unique operational challenges. METLRG SOLUTIONS develops equipment that addresses specific requirements while ensuring efficiency and reliability.
Screw Conveyors for Controlled Material Movement
Screw conveyors are ideal for transporting powders, granules, and semi-solid materials in a controlled manner.
Industries commonly using screw conveyors include:
Chemical manufacturing
Food processing
Pharmaceuticals
Cement production
Their enclosed design helps reduce material contamination and environmental exposure.
Ash Conditioners for Dust-Free Ash Handling
Power plants and industrial boilers generate significant quantities of ash. Effective ash conditioning is essential for safe handling and environmental compliance.
METLRG SOLUTIONS manufactures ash conditioners that:
Reduce airborne dust
Improve handling efficiency
Support environmental safety requirements
Enhance operational cleanliness
These systems contribute significantly to sustainable industrial operations.
Roller Conveyors for Efficient Product Movement
Roller conveyors are widely used in assembly lines, packaging facilities, warehouses, and logistics operations.
Their advantages include:
Reduced manual labor
Improved workflow efficiency
Flexible integration with automation systems
Enhanced productivity
METLRG SOLUTIONS offers roller conveyor solutions tailored to diverse industrial applications.
Precision Flow Control Systems for Industrial Operations
Beyond conveying equipment, industrial facilities often require precise control over material flow. This is where specialized gate systems become essential.
Sector Gates
Sector gates are commonly used to regulate bulk material discharge and flow control. Their robust construction ensures reliable operation even under demanding conditions.
Rack & Pinion Gates
Designed for accurate and smooth operation, rack & pinion gates provide excellent control over material handling processes. Their mechanical precision makes them suitable for industries where controlled discharge is critical.
Rod Gates
Rod gates offer dependable performance in applications requiring controlled material isolation and discharge. They are engineered for durability and ease of operation.
Together, these gate systems help industries maintain process efficiency while reducing operational disruptions.
Conveyor Spares That Support Long-Term Equipment Performance
A conveyor system is only as reliable as its components. Regular maintenance and timely replacement of worn parts are essential for uninterrupted operations.
METLRG SOLUTIONS supplies quality conveyor spares that help customers:
Extend equipment life
Minimize downtime
Improve operational efficiency
Reduce maintenance costs
By ensuring the availability of critical spare parts, the company supports long-term equipment reliability across industries.
Serving Industries with Customized Engineering Solutions
No two industrial facilities operate exactly the same way. Material characteristics, production volumes, environmental conditions, and operational goals vary significantly from one project to another.
METLRG SOLUTIONS understands these differences and focuses on delivering customized solutions tailored to specific customer requirements.
Its equipment serves a wide range of sectors, including:
Power Generation
Cement Manufacturing
Steel Industries
Mining Operations
Chemical Processing
Fertilizer Plants
Infrastructure Projects
Warehousing and Logistics
This diverse industry experience enables the company to provide practical and effective material handling solutions.
Digital Visibility and Industry Networking
In today's interconnected business environment, customers increasingly search for reliable industrial suppliers through digital platforms. To enhance accessibility and industry visibility, METLRG SOLUTIONS has listed its products and business on BONC Network, a platform where businesses showcase their products and services to potential customers and industry buyers.
Such visibility helps industrial purchasers discover suitable equipment suppliers while enabling businesses to strengthen their market presence.
Building Long-Term Value Through Quality and Innovation
Industrial equipment investments are expected to deliver performance over many years. Reliability, engineering quality, and operational efficiency are factors that influence purchasing decisions.
METLRG SOLUTIONS continues to focus on:
Quality manufacturing standards
Robust engineering practices
Customer-centric solutions
Reliable after-sales support
Continuous product improvement
The company's commitment to delivering dependable material handling equipment has helped it support industries that require consistent performance under demanding operating conditions.
Additionally, its presence on BONC Network enables industry professionals and buyers to explore its product offerings more conveniently, creating opportunities for collaboration and business growth.
Conclusion
Efficient material handling systems form the backbone of modern industrial operations. From Belt Conveyors and Bucket Elevators to Chain Conveyors, Screw Conveyors, Ash Conditioners, Roller Conveyors, Sector Gates, Rack & Pinion Gates, Rod Gates, and Conveyor Spares, every component contributes to productivity, safety, and operational success.
With a broad product portfolio, industry-focused engineering expertise, and a commitment to quality, METLRG SOLUTIONS continues to provide solutions that help industries move materials efficiently and achieve long-term operational excellence. As businesses seek reliable partners for material handling requirements, METLRG SOLUTIONS remains equipped to meet evolving industrial demands with performance-driven solutions.